Shaft Journal Grinding: Design and Process Decisions
Home
/
Blog
/
Shaft Journal Grinding: Design and Process Decisions
Shaft Journal Grinding: Design and Process Decisions
October 26, 2026
Table of Contents
Shaft journal grinding is a practical engineering decision for buyers responsible for precision shaft journals. This guide focuses on centers, journal form, grinding relief, connecting these details to the drawing, manufacturing route and first-article review.
Shaft journal grinding: start with the assembled function
A useful shaft journal grinding plan begins with what the component must do after installation. For precision shaft journals, write down the mating interfaces, the direction of the working load and the surfaces that establish position. A drawing that treats every face as equally important often makes inspection more expensive without clarifying whether the part will work. Separate the functional envelope from incidental shape before asking a supplier to recommend a route.
Center condition and support alignment can create journal errors even when the wheel produces a fine finish.
For shaft journal grinding, the first design review should therefore connect each critical requirement to a visible feature. Ask what would happen if that feature were at either limit of its tolerance. If the answer depends on the mating part, include that information in the review rather than leaving the supplier to infer it from a single component model.
Shaft journal grinding: turn the design intent into clear drawing requirements
Identify the functional axis, journal tolerances and shoulder relationships. Provide grinding relief where needed and define the state of any center holes used by the process.
The drawing and model for shaft journal grinding need a clear order of precedence. Identify the revision, units and general tolerances, then call out exceptions at the feature itself. Do not rely on a shaded CAD image to communicate a surface requirement, an assembled condition or a material treatment. Those details can change the route even when the visible shape remains identical.
When reviewing precision shaft journals, distinguish a maximum permissible envelope from a target manufacturing value. The supplier should understand which changes need engineering approval. A proposed radius, relief or access hole may make production easier, but its effect on strength, sealing, motion or interchangeability still belongs in the design decision.
Shaft journal grinding: choose references that survive the manufacturing route
Reference and access review
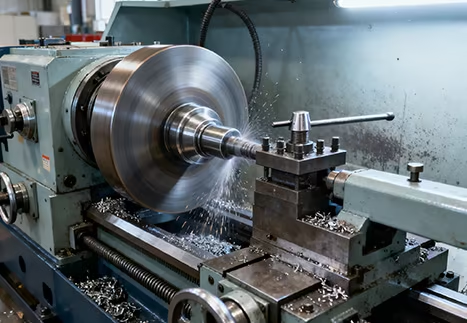
A reference scheme for shaft journal grinding should be usable during production and meaningful during final inspection. Start from the surfaces that locate precision shaft journals in the assembly. Review whether those surfaces exist at the first operation and whether later work will change them. Where temporary references are needed, explain how the route transfers to the finished functional references.
Clamping and locating serve different purposes in shaft journal grinding. Locators establish position; clamps keep the part supported against the process forces. An arrangement that pulls a flexible part into shape may produce a convincing result in the fixture and a different result after release. State the condition in which acceptance measurements are required.
Ask for a setup sketch when the relationship is difficult to understand. It should show contact locations, the direction of restraint and access to the critical features. The sketch does not need to reveal proprietary programming details to be useful. Its purpose is to resolve the physical assumptions that affect the finished interface.
Shaft journal grinding: match geometry to process access
Coordinate pre-grinding allowance and heat-treatment condition. Inspect centers, support the shaft appropriately and plan wheel dressing and coolant delivery for the finish requirements.
For shaft journal grinding, consider the complete tool and fixture envelope rather than the cutting tip alone. A feature may be reachable in CAD but blocked by a clamp, neighboring wall or machine component. Review access to the deepest or most restricted area before relaxing a useful tolerance elsewhere. Moving one nonfunctional feature can be more effective than selecting a more elaborate machine.
An economical route for precision shaft journals should also leave access for cleaning and inspection. Features that become inaccessible after assembly need a defined verification point earlier in the route. This avoids discovering at final inspection that an important internal requirement cannot be checked without disassembly or sectioning.
Shaft journal grinding: separate geometry, finish and material condition
Treat material condition, dimensional geometry and surface condition as separate decisions in shaft journal grinding. A smooth surface can still be out of position. A correctly located feature can still have a damaged edge. A certificate for incoming material does not automatically describe the condition after thermal processing, joining or finishing.
For precision shaft journals, mark the surfaces that need special protection and the edges that affect assembly. Where a coating or treatment changes size, define whether the drawing limit applies before or after that operation. Include any masking requirement explicitly. This gives the supplier a way to plan allowance without guessing which dimensions should be adjusted.
A shaft journal grinding review should avoid copying an exceptional capability figure onto every feature. Achievable results depend on size, geometry, restraint, material and the full route. Ask the supplier to evaluate the actual requirement and identify any limitation before price or delivery becomes the only subject of discussion.
Shaft journal grinding: compare design options before the first build
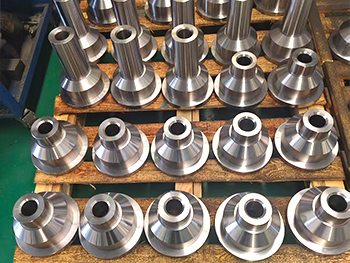
The practical choice in shaft journal grinding is often between retaining a difficult feature, changing a nonfunctional detail or accepting an additional operation. Compare those options using the same assembly requirement. A cheaper process is not an improvement if it transfers adjustment work or uncertainty to the customer.
Use the comparison below to decide what belongs in the first review of precision shaft journals. Request a written explanation for a proposed change, including the affected feature and the condition it is intended to improve. Keep the approved drawing as the common reference once a decision is made.
| Feature or decision | Design consideration | Inspection focus | RFQ information |
|---|---|---|---|
| Centers | Preserve the functional reference | Inspect centers and axis relationship | Identify allowed support method |
| Journal form | Control size and form separately | Measure multiple axial positions | Request form and runout results |
| Grinding relief | Provide tool access at shoulders | Inspect transitions and edge condition | Show relief geometry |
Use a first article to test the uncertain assumption
Illustrative troubleshooting situation
A journal fits a ring gauge but vibrates in rotation. Review form and runout from the functional axis instead of treating size as the only condition.
For shaft journal grinding, use the first article to answer a specific question: does the selected geometry, reference scheme and route produce the required interface? Choose measurements or a fit trial that address that question. A sample made under exceptional conditions is useful for development, but it should not be treated as proof that the production route is stable.
Record what the first build taught you about precision shaft journals, including any drawing change or process dependency. If the supplier changes the setup, material condition or finish after the trial, decide which evidence needs to be repeated. Keep successful trial measurements linked to the exact revision that produced them.
Shaft journal grinding: release a complete manufacturing package
Measure journal size, roundness and runout as distinct characteristics. Check multiple axial locations where taper or barrel shape may affect the bearing fit.
Before releasing shaft journal grinding, check that the package contains the model, drawing, material condition, quantity, critical characteristics and expected inspection evidence. Include known mating constraints and any customer approval points. This is more useful than an open-ended instruction to make the part as accurately as possible.
The final shaft journal grinding decision should leave both parties able to explain what constitutes an acceptable component. Review unresolved assumptions before ordering the full quantity. If a requirement remains uncertain, identify the trial or engineering decision that will close it instead of hiding the uncertainty in a general note.
Prepare your project for a technical review
Apex lists Grinding Services among its manufacturing services. Send the drawing and requirements for your precision shaft journals to discuss the actual scope. Use the material overview as a starting point, then confirm the grade, condition and project-specific feasibility in the quotation.
For further process background, see Norton industrial abrasive technical guidance. Apply tooling or joining guidance to the actual material and setup with the responsible manufacturing team. These references do not replace the approved component drawing or an application-specific qualification.
For a focused shaft journal grinding discussion, send the current model and drawing, quantity, material condition, critical interfaces and required delivery window through the form below. Identify the main uncertainty described in this guide so the engineering review can address it directly. Contact Apex Precision to request a project review and quotation.
Frequently asked questions
What is the main risk in shaft journal grinding?
Center condition and support alignment can create journal errors even when the wheel produces a fine finish. Review this risk against the actual geometry and mating interfaces before selecting tolerances.
What drawing information is needed for shaft journal grinding?
Identify the functional axis, journal tolerances and shoulder relationships. Provide grinding relief where needed and define the state of any center holes used by the process.
Can shaft journal grinding use a standard process route?
Coordinate pre-grinding allowance and heat-treatment condition. Inspect centers, support the shaft appropriately and plan wheel dressing and coolant delivery for the finish requirements. The final route needs review against the actual drawing and quantity.
Which checks should be planned before production?
Measure journal size, roundness and runout as distinct characteristics. Check multiple axial locations where taper or barrel shape may affect the bearing fit.
When should a design change be approved?
Approve a change before the supplier incorporates it into the first article or production lot. Record its effect on the mating interface, material condition and acceptance requirements, then update the controlled revision.
Latest News
Contact Us
FAQ
What types of parts can be machined?
We can machine a wide range of high-precision CNC parts for automotive, aerospace, medical devices, industrial machinery, and automation equipment, including complex geometries and custom non-standard parts.
What is the machining accuracy?
We can achieve high-precision machining with ±0.005mm tolerance and ensure consistent quality through our strict quality control system.
Can you provide small-batch and prototype manufacturing services?
Yes, we support small-batch production and prototype machining, with flexible scheduling to meet urgent client requirements.
Do you offer customized processing solutions?
Yes, we provide customized solutions with one-on-one technical support, from design review and process optimization to final machining.
How long does delivery usually take?
Delivery time depends on part complexity and quantity, typically within 1-6 weeks. We provide a detailed schedule upon order confirmation.
What certifications are available for quality management systems?
We hold ISO 9001, ISO 14001, and ISO 45001 certifications, strictly following international quality, environmental, and safety standards.
How long does delivery usually take?
Delivery time depends on part complexity and quantity, typically within 1-6 weeks. We provide a detailed schedule upon order confirmation.