
Metal Machining Explained: Processes, Materials and Quality
Home
/
Blog
/
Metal Machining Explained: Processes, Materials and Quality
Metal Machining Explained: Processes, Materials and Quality
August 19, 2026
Table of Contents
Introduction
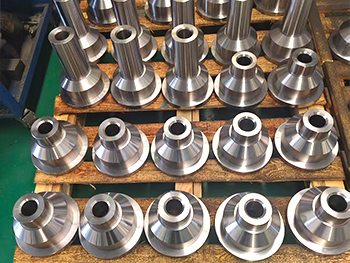
Metal machining is one of the fundamental ways of turning raw metal, castings, forgings and preformed blanks into functional engineering components. A finished shaft, housing, bracket, flange or machine component may appear to be defined primarily by its shape, but achieving that shape consistently requires a coordinated combination of material selection, cutting strategy, workholding, tooling, tolerance control and inspection.
Modern machining equipment can create complex geometry with a high degree of repeatability, yet machine capability alone does not determine the quality of the finished part. A technically correct CNC program can still produce dimensional variation when a workpiece moves in its fixture, a cutting tool wears, a thin wall deflects or thermal conditions change during a long machining cycle. For this reason, reliable metal machining should be understood as a complete manufacturing process rather than simply the movement of a cutting tool.
For engineers and product developers, this broader perspective is useful because many machining problems begin before the first operation starts. Material, geometry, tolerance strategy and datum selection can either support stable manufacturing or create unnecessary difficulties that later need to be compensated for through additional setups and process adjustments.
What Is Metal Machining?
Machining is a subtractive manufacturing process in which material is removed from a workpiece to create the required dimensions, surfaces and geometry. In metal machining, this principle is applied to metallic workpieces using operations such as milling, turning, drilling, boring, reaming and grinding, with the specific process selected according to the shape and functional requirements of the component.
The starting material does not always need to be solid billet or bar. Many metal machining projects begin with castings or forgings that already contain much of the required near-net geometry. CNC machining is then used selectively to establish important bores, mounting faces, threaded holes, sealing surfaces and other precision interfaces.
This distinction is important because machining should not automatically be used to create every surface from raw stock. A practical manufacturing route determines which geometry can be established efficiently by the starting process and which features require the greater dimensional control available through machining.
Metal machining is therefore best viewed as the link between raw material condition and finished functional geometry. The process removes material where necessary while preserving the characteristics that the component needs for assembly and service.
CNC Milling in Metal Machining
CNC milling is widely used when metal components contain flat surfaces, pockets, slots, hole patterns, contours or features distributed across several faces. A rotating cutting tool removes material while controlled machine movements determine the relationship between the cutter and the workpiece.
The complexity of a milling process depends heavily on part geometry. A relatively simple plate with holes and external contours may require only straightforward machining orientations, while a housing containing deep pockets, angled surfaces and features on several sides can require more advanced setup planning or multi-axis machining.
Tool access is one of the main considerations. Deep cavities require longer cutters, and increased tool extension generally reduces rigidity. Very small internal radii can also require smaller tools, which may make cutting conditions more sensitive to vibration or deflection. For this reason, design choices that appear minor in CAD can have a significant effect on machining strategy.
Milling is most effective when important features are grouped around practical machining directions and meaningful datums. When several related surfaces can be produced from the same stable reference condition, the process can maintain their geometric relationship more directly.
CNC Turning for Rotational Metal Components
CNC turning is naturally suited to metal parts whose main geometry is organized around a rotational axis. Shafts, bushings, sleeves, rollers, pins, couplings and many flange-type parts can be produced by rotating the workpiece while cutting tools remove material from external or internal surfaces.
Several operations can often be completed while the component remains referenced around the same spindle axis. External diameters, shoulders, grooves, threads and internal bores may therefore maintain a strong geometric relationship when the process is planned correctly.
Long or slender workpieces require additional consideration because cutting forces can cause the component to deflect. The machine can position the tool correctly while the workpiece itself moves slightly away from the cutter, resulting in dimensional or surface variation. Suitable support, cutting conditions and machining sequence can help manage this behavior.
Turning should therefore not be evaluated only by whether a component is cylindrical. The functional relationship between its diameters, faces and internal features should determine whether turning is the primary manufacturing process.
Milling and Turning Often Work Together
Many real metal components cannot be classified purely as milled or turned parts. A shaft may contain flats, cross holes or slots, while a machined housing can include precision bores and cylindrical features. In these cases, an effective metal machining strategy combines processes according to the geometry each produces most naturally.
The order of operations matters because one process may establish the datum required by another. A turned diameter can become a locating feature for subsequent milling, while a milled face may provide a stable reference for later boring or drilling.
The objective is not to minimize the number of process types used. Instead, manufacturing engineers should minimize unnecessary transitions while ensuring that important feature relationships remain stable throughout production.
Integrated CNC machining services can combine turning, milling and multi-axis processing around a common process plan, which is particularly useful when a component contains both rotational and prismatic geometry.
Material Selection Changes the Metal Machining Process
Different metals behave differently when they are cut, so material selection affects much more than the final mechanical properties of the component. Hardness, strength, thermal conductivity, rigidity and alloy condition can influence cutting forces, tool wear, chip behavior and dimensional stability.
Aluminum alloys are frequently machined when relatively low weight and good machinability are desirable. Steels can support components requiring strength and wear performance, while stainless steels may be selected when corrosion-related characteristics are important. Other alloys can introduce additional machining considerations depending on their mechanical and thermal behavior.
The exact strategy should be developed around the material rather than transferred automatically from another project. Tool geometry, cutting conditions, coolant strategy and workholding may all change even when two components have similar geometry.
Starting material form is another consideration. Bar and plate provide relatively predictable external reference surfaces, while castings and forgings can contain greater dimensional variation before machining. The first operation on a near-net blank therefore needs a suitable datum strategy so later precision features are not referenced from unstable surfaces.
Material selection and machining planning should consequently begin together rather than being treated as unrelated engineering decisions.
Castings and Forgings Require Different Machining Planning
Many metal components begin as cast or forged blanks rather than rectangular billets or round bars. These near-net processes can create much of the overall geometry before CNC machining begins, reducing unnecessary material removal and allowing ribs, bosses, curved surfaces and other structural features to be incorporated into the starting workpiece.
However, near-net blanks also introduce additional metal machining considerations because their initial surfaces may contain greater variation than finished CNC features. Sufficient machining allowance needs to remain around critical interfaces, while locating and fixturing strategies should account for the actual condition of the blank. Once stable machined datums have been established, later operations can use those references to control more demanding dimensions and geometric relationships.
A strong process plan therefore identifies which features originate from casting or forging and which will ultimately be established through CNC machining. This prevents unnecessary precision requirements from being applied to general near-net surfaces while concentrating machining control on the interfaces that influence final assembly and performance.
Functional Datums Create a Stable Reference System
Datums connect part design with manufacturing and inspection by defining the references from which important features are located. When a datum reflects the way a component interacts with its final assembly, it becomes easier to develop machining setups around the same functional relationship.
For example, if a housing is located in service by a mounting face and a central bore, those features may be more meaningful machining references than an unrelated external contour. Subsequent holes, pockets and surfaces can then be controlled relative to the geometry that actually determines assembly position.
Poor datum selection can create unnecessary uncertainty. A component may be machined from one group of surfaces and inspected from another, making it difficult to determine whether an apparent positional difference comes from the process or simply from inconsistent referencing.
A reliable metal machining strategy therefore identifies functional references before tooling and fixture decisions are finalized. This creates a common geometric language between design, machining and quality control.
Tolerances Should Protect Function
Tolerance defines how much dimensional or geometric variation can be accepted while the component continues to function correctly. In metal machining, the most effective tolerance strategy does not attempt to make every dimension as restrictive as possible.
Bearing seats, locating diameters, sealing interfaces and alignment features may require close control because variation directly affects assembly or movement. Non-functional external geometry or clearance surfaces can often accept more variation without changing component performance.
Applying unnecessarily restrictive tolerances everywhere can make machining and inspection more difficult without improving the product. Smaller allowable variation may require more controlled setups, additional finishing operations or more frequent measurement even when the feature provides little functional value.
The correct approach is therefore to ask what each tolerance protects. When variation can cause interference, leakage, poor alignment or unstable motion, the requirement deserves close attention. When the same variation has little effect on function, the tolerance can usually be selected with greater manufacturing practicality.
Workholding Is Central to Metal Machining Accuracy
Every machining operation requires the workpiece to be located and held securely. If that relationship changes during cutting, programmed machine movement cannot guarantee that the finished feature remains in the intended position.
A fixture must resist cutting forces while allowing the tool to reach the necessary surfaces. At the same time, clamping should not unnecessarily deform thin walls, slender components or other flexible geometry.
This balance becomes especially important for complex metal parts. Excessive clamping pressure can temporarily distort a workpiece, causing it to appear correct while restrained but change shape after the fixture is released. Insufficient restraint creates the opposite problem because the component can move under cutting forces.
Workholding also changes throughout the manufacturing route. Raw material may provide convenient initial surfaces that disappear after rough machining, so controlled datum features need to be created before those original references are removed.
Good metal machining therefore treats fixture design as part of process engineering rather than simply a setup activity immediately before cutting.
Tool Selection Influences Accuracy and Surface Quality
Cutting tools determine how the machine physically interacts with the metal. Their diameter, length, geometry, material and condition all influence cutting forces and the quality of the resulting surface.
Rigid tooling generally provides a more stable cutting condition than long or slender tooling. Deep pockets, narrow features and difficult internal geometry can require increased tool extension, making vibration and deflection more important considerations.
Tool wear introduces gradual variation during repeated machining. A cutting edge changes as it removes material, and this can influence dimensions, surface texture and the amount of force acting on the workpiece.
For this reason, tooling should be managed throughout production rather than selected once during programming and then treated as a fixed variable. Critical dimensions may need periodic inspection so gradual wear can be identified before it produces unacceptable components.
The strongest tool strategy therefore balances geometry, material, cutting conditions and expected production requirements.
Roughing and Finishing Serve Different Purposes
Rough machining and finishing should often be considered separate stages because they have different objectives. Roughing removes a larger volume of unwanted material and creates an approximate form, while finishing establishes final dimensions and surfaces under more controlled cutting conditions.
This separation becomes particularly valuable when large amounts of metal are removed. Heavy cutting can introduce greater forces and heat, while the changing shape of the workpiece can alter its rigidity as the operation progresses.
Leaving a controlled amount of material for finishing allows the final surfaces to be created after most major material removal has already occurred. Critical features can then be machined under conditions better suited to dimensional and surface control.
Not every part requires an elaborate roughing and finishing strategy, but treating them as distinct objectives gives manufacturing engineers greater flexibility when precision and stability are important.
Thermal Conditions Can Affect Metal Machining
Cutting generates heat, and the workpiece, tool and machine structure can all experience temperature changes during machining. Because metals expand and contract with temperature, these conditions can influence dimensional results when tolerances become demanding.
Heavy roughing and long machining cycles can produce different thermal conditions from light finishing. A component inspected immediately after intensive material removal may also be in a different condition from the same part after temperature has stabilized.
The importance of this effect depends on material, part size, machining sequence and required accuracy. General components may not require significant thermal consideration, while precision interfaces can be more sensitive to inconsistent conditions.
Manufacturers can manage this by maintaining stable process conditions where practical, separating heavy removal from critical finishing when necessary and considering when important dimensions are measured.
Thermal stability should therefore be treated as one possible source of machining variation rather than ignored until unexplained dimensional changes appear.
Surface Finish Is Not the Same as Dimensional Accuracy
A machined surface can satisfy dimensional tolerance while still having a texture unsuitable for its intended function. Surface finish should consequently be specified independently of size when it affects sealing, sliding, bearing contact or another mechanical interface.
Tool geometry, cutting conditions, feed, vibration and tool wear all influence surface quality. This means a component can remain dimensionally acceptable while its surface gradually changes as the cutting tool deteriorates.
Not every machined surface needs the same level of finish. A sealing face may justify additional process control, while a non-contact pocket or general clearance surface may perform correctly with the normal finish produced by the selected machining operation.
Grinding or other secondary processes can also be used where final surface or dimensional requirements are better achieved after primary milling or turning. These operations should be planned in advance so appropriate material allowance remains available.
Secondary Machining Processes Complete the Part
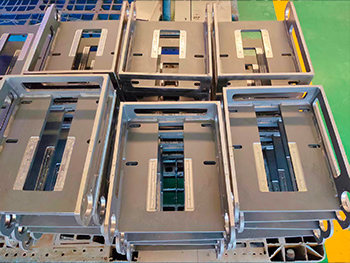
Metal machining can involve more than primary milling and turning. Drilling, reaming, boring, tapping and grinding may all form part of the manufacturing route depending on the geometry and functional requirements of the component.
Boring and reaming can provide controlled internal geometry where a drilled hole alone does not meet the final requirement. Tapping creates threaded interfaces, while grinding can be used on selected surfaces requiring additional dimensional or finish control.
The process sequence should determine when these operations occur. If a precision bore must maintain a close relationship with a mounting face, both features need to be planned around meaningful datums rather than treated as unrelated secondary operations.
The same principle applies when welded, cast or forged components require final machining. Secondary processes should complete the functional geometry of the part rather than simply being added after the main CNC cycle without reference to the overall design.
Multi-Axis Machining Can Reduce Setup-Related Variation
Complex metal parts often contain features distributed across several sides. Conventional processing may require the workpiece to be removed and repositioned several times before every surface can be reached.
Each repositioning operation creates another reference condition. If critical features are produced in different setups, their final relationship depends partly on how accurately the workpiece is relocated.
Multi-axis machining can reduce some of these transitions by allowing the cutting tool to approach the workpiece from additional directions while the component remains under a controlled reference condition.
The main benefit is not simply the ability to produce complicated shapes. Multi-axis processing can also help preserve feature relationships by reducing unnecessary manual repositioning.
However, additional machine axes should be used because the geometry justifies them, not because a more complex machine is automatically better. A simpler process with strong tool access and stable workholding can remain the best solution for many metal machining projects.
Quality Control Should Begin Before Final Inspection
Final inspection can determine whether a completed component satisfies its drawing, but waiting until machining is finished means any variation is discovered only after all manufacturing effort has already been invested.
In-process measurement provides earlier information. A critical bore can be checked before later features are added, while an important datum surface can be verified before it becomes the reference for additional machining.
This makes it easier to identify where variation enters the process. Gradual dimensional movement may indicate tool wear, while sudden positional changes can point toward a setup or fixture issue.
Inspection should therefore support process control rather than act only as a final sorting stage. Measurement results provide evidence that can be used to adjust manufacturing before the same problem affects more parts.
The following table summarizes several important metal machining variables and their influence on finished components:
| Process Area | Main Manufacturing Concern | Practical Control Approach |
|---|---|---|
| Material selection | Different cutting and thermal behavior | Match tooling and parameters to the actual material |
| Starting blank | Variation in cast or forged geometry | Establish reliable first-operation datums |
| Tolerances | Unnecessary manufacturing restrictions | Apply close control to functional features |
| Workholding | Movement or deformation | Use stable locating with suitable clamping force |
| Tool rigidity | Deflection and vibration | Maintain practical tool access and extension |
| Tool wear | Gradual dimensional drift | Monitor tool condition and critical dimensions |
| Roughing | Cutting force and material movement | Leave suitable allowance for finishing |
| Temperature | Dimensional variation | Maintain stable conditions for critical operations |
| Surface finish | Interface performance | Specify finish according to actual function |
| Setup changes | Feature relationship errors | Group related geometry where practical |
| Inspection | Late identification of variation | Use in-process checks for critical characteristics |
This framework illustrates why successful metal machining depends on a controlled system rather than any single machine setting.
DFM Can Improve Metal Machining Before Production Starts
Design for manufacturability allows machining risks to be identified while geometry can still be changed relatively easily. Features that look straightforward in CAD may require difficult tooling, unstable workholding or additional setups once physical manufacturing is considered.
Extremely small internal radii can restrict cutter selection, while deep narrow pockets may require long tools with reduced rigidity. Very thin walls can move during machining, and minor features placed on several unrelated faces can increase setup count without providing additional functional value.
DFM does not mean simplifying every component. Complex geometry should remain when it is necessary for performance or assembly. The purpose is to distinguish required complexity from manufacturing difficulty that can be removed without changing what the part needs to do.
Early manufacturing review can therefore improve process stability before programming, fixture design and machining have already committed the project to a difficult route.
Prototype Metal Machining Should Develop the Process
Prototype machining provides more than the first physical sample of a component. It reveals how the actual material, tooling, fixture and geometry behave together under cutting conditions.
An early part may show that a thin wall requires a different operation sequence, a deep cavity needs more rigid tooling or a particular datum is difficult to reproduce reliably. These findings should become part of process development rather than remaining temporary adjustments made only to complete the first component.
Programs can be revised, fixtures can be improved and inspection points can be moved according to the information collected during prototype manufacturing. When the component later enters repeated production, the process should already reflect these lessons.
A successful prototype proves that the geometry can be produced. A mature metal machining process demonstrates that the required geometry can be reproduced consistently.
Moving From Prototype to Repeatable Metal Machining
Repeated production introduces conditions that may not be obvious during the first few parts. Cutting tools wear, fixtures are loaded repeatedly, raw materials can vary within their specified condition and machines operate for longer periods.
A stable production process needs controls that account for these changing variables. Workholding should reproduce the same reference system, tooling strategies should include appropriate monitoring and inspection should focus on characteristics that reveal meaningful process change.
Process documentation also becomes more important. If a particular machining sequence or adjustment is necessary to maintain one critical feature, that information should become part of the established manufacturing route rather than remain only with one experienced operator.
Repeatability is therefore one of the best tests of metal machining quality. Producing one highly accurate component demonstrates technical capability, while maintaining functionally acceptable results over continued manufacturing demonstrates process stability.
Common Metal Machining Problems and Their Causes
Dimensional variation can originate from tool wear, material movement, fixture instability, temperature or incorrect reference conditions. Poor surface quality can result from cutting-edge deterioration, vibration, chip interference or unsuitable machining parameters, while positional problems may appear when features are divided across unstable setups.
Burr formation is another common issue, particularly around intersecting holes, slots and machined edges. Deep cavities and slender tooling can introduce vibration, while thin walls may move under cutting forces even when the machine follows the programmed path accurately.
These conditions should be investigated through root-cause analysis rather than corrected only through repeated offset changes. If the same dimension gradually moves in one direction, tool condition may deserve attention. If one group of features changes after a specific setup, the locating strategy may be more important than the cutting program.
Reliable machining improves when inspection information is used to understand why variation occurs rather than simply to separate acceptable and unacceptable finished components.
How to Evaluate a Metal Machining Manufacturer
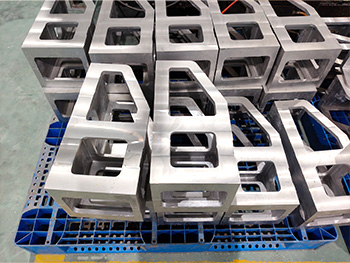
A suitable metal machining manufacturer should first be able to understand the functional requirements shown on the drawing. Equipment capability is important, but milling machines, lathes and multi-axis machining centers provide value only when they are combined with appropriate workholding, tooling and inspection.
Material experience should match the project because cutting behavior changes significantly between different metals and starting forms. A manufacturer machining castings or forgings should also understand machining allowance and datum development rather than treating those blanks like conventional billet.
Inspection capability should correspond to the actual tolerances and geometric relationships on the drawing. For repeated production, process monitoring and documentation are also important because the objective is not simply to manufacture one successful sample.
Technical communication provides another useful indicator of manufacturing maturity. When a drawing contains poor tool access, unstable walls or unnecessarily restrictive requirements, an experienced manufacturing team should be able to identify those risks during review and explain their manufacturing implications clearly.
Conclusion
Metal machining is a coordinated manufacturing process that transforms raw stock, castings, forgings and other blanks into functional engineering components through controlled material removal. CNC milling and turning provide the main cutting capability, while drilling, boring, grinding and other secondary processes complete features that require additional control.
The quality of the finished component depends on far more than CNC positioning. Material behavior influences cutting and dimensional stability, datums connect part function to machining setups, workholding determines whether each workpiece enters the process consistently and tool condition changes throughout production.
Tolerance and surface specifications should therefore be based on actual function. Precision should be concentrated on the features that affect fit, movement, sealing and alignment instead of being applied unnecessarily to every dimension.
Inspection completes the process by providing evidence about manufacturing stability. When measurement results are used during production rather than only at the end, they can identify tool wear, setup problems and process drift before the same variation affects additional components.
A strong metal machining strategy ultimately connects design, material, machining and quality control through one functional process plan. When these elements work together, complex metal parts become easier to manufacture consistently, verify reliably and reproduce across repeated production.
FAQ
What is metal machining?
Metal machining is a subtractive manufacturing process that removes material from a metal workpiece to create required dimensions, surfaces and geometry. Common methods include CNC milling, turning, drilling, boring and grinding, with the process selected according to material, part shape and functional requirements.
What metals can be used for metal machining?
Metal machining can be applied to aluminum alloys, steels, stainless steels and many other machinable alloys. The correct cutting strategy depends on hardness, rigidity, thermal behavior and material condition, so tooling, cutting parameters and workholding should be selected for the actual workpiece.
What is the difference between CNC milling and CNC turning?
CNC milling normally uses rotating cutting tools to create pockets, surfaces, holes and prismatic geometry, while CNC turning rotates the workpiece and is particularly suitable for shafts, bushings, sleeves and other rotational parts. Complex components may require both processes within one manufacturing route.
What factors affect metal machining accuracy?
Metal machining accuracy depends on machine condition, material behavior, functional datums, fixture stability, cutting-tool rigidity, tool wear, thermal conditions and inspection. Reliable production requires these factors to be controlled together rather than depending only on the programmed position of the CNC machine.
How can metal machining parts be designed for better manufacturability?
Metal parts can be easier to machine when designers provide practical internal radii, sufficient tool access, stable wall geometry, clear functional datums and suitable tolerances. Workholding and inspection access should also be considered early so the part can be manufactured consistently rather than only produced once.
Latest News
Contact Us
FAQ
What types of parts can be machined?
We can machine a wide range of high-precision CNC parts for automotive, aerospace, medical devices, industrial machinery, and automation equipment, including complex geometries and custom non-standard parts.
What is the machining accuracy?
We can achieve high-precision machining with ±0.005mm tolerance and ensure consistent quality through our strict quality control system.
Can you provide small-batch and prototype manufacturing services?
Yes, we support small-batch production and prototype machining, with flexible scheduling to meet urgent client requirements.
Do you offer customized processing solutions?
Yes, we provide customized solutions with one-on-one technical support, from design review and process optimization to final machining.
How long does delivery usually take?
Delivery time depends on part complexity and quantity, typically within 1-6 weeks. We provide a detailed schedule upon order confirmation.
What certifications are available for quality management systems?
We hold ISO 9001, ISO 14001, and ISO 45001 certifications, strictly following international quality, environmental, and safety standards.
How long does delivery usually take?
Delivery time depends on part complexity and quantity, typically within 1-6 weeks. We provide a detailed schedule upon order confirmation.